Proof,
not promises.
Design validation, process capability and 100% electrical test are one system at PANAWIN — not three separate departments.
The quality system
Quality is designed in, then verified.
It begins with material selection and construction design. It continues through process capability studies, first-article inspection and 100% test. It does not end until the production reel performs like the sample.
Four disciplines
One test floor. The full operating envelope.
Electrical, mechanical, environmental and material analysis sit together in-house. That means a failure can move from observation to root cause without leaving the building.
Design validation
Construction review, material selection, simulation and prototype testing against the application envelope.
Process capability
DOE, PFMEA, control plans and Ppk studies for critical characteristics, including high-speed SI.
100% electrical test
Continuity, withstand voltage, insulation resistance and application-specific test programs.
Traceability
Lot-level records connect raw material, process parameters, test results and shipment.
Testing capability
Thirty-nine ways to find the problem first.
Our in-house test matrix covers the electrical, mechanical, environmental and material performance of cables and harnesses — from conductor resistance to six-axis robot dress-pack testing.
Electrical
- High-frequency testing
- Conductor resistance
- Contact resistance
- Thermal rise test
- Smoke test
- Current carrying test
- Withstand voltage
- Insulation resistance
- Voltage drop
- Withstand & partial discharge
- Shielding transfer impedance
- Harness test station
Mechanical
- Dimensional measurement
- Mechanical property
- Tensile / pull-off / pressure
- Insertion & extraction
- Bending test
- 3D torsion test
- Torsion test
- Flexure test
- Drag chain test
- Torsional test for wind
- Six-axis robot harness test
- Robotics dress-pack test
Environmental
- Salt spray test
- Constant temperature & humidity
- Low temperature test
- Low-temperature winding
- Low-temperature tensile
- Low-temperature impact
- High-temperature test
- Thermal cycling test
Material & other
- Coating film thickness
- Flame retardant test
- Terminal cross-section
- Waterproof test
- Seal integrity test
- RoHS tester
- Infrared spectroscopy analysis
Measurement & management
Capability you can measure.
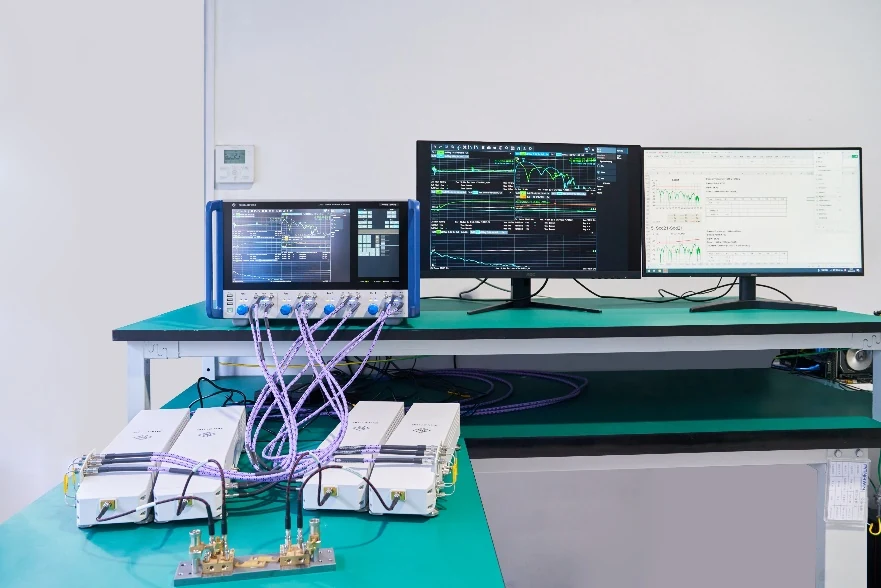
High-speed cable performance is only meaningful when it is measured at the right frequency, on the right sample size and over a full reel. Our lab is equipped for both development and serial qualification.
Equipment list reflects the high-speed cable laboratory. Additional electrical, mechanical and environmental test equipment supports the wider product portfolio.
Certification
Audited systems. Certified products.
Nine management-system and verification standards, plus a broad UL product-safety portfolio, support automotive, medical, industrial and data-center programmes.
Standards-led assembly discipline.
PANAWIN is a member in good standing of IPC, supporting the cable and harness assembly standards that customers rely on.
Qualified for high-voltage installation.
Our teams hold high-voltage cable jointer and installation qualifications for demanding energy and infrastructure programmes.
UL portfolio
Coverage across cable, wire and assemblies.
Fifteen UL standards underpin our product-safety coverage for industrial, automotive, data-center, photovoltaic and appliance applications.
Production qualification
224G capability, proven over a full reel.
Duration study and process-capability study for SI, length > 1,500 ft (one full reel), 32 pieces. Tape dimension, structure, overlap and lay length verified within specification on 16 pieces.